Gaskets · Made to order
Sanitary Tri-Clamp (Ferrule) Gaskets — Moulded to Your Clamp Standard
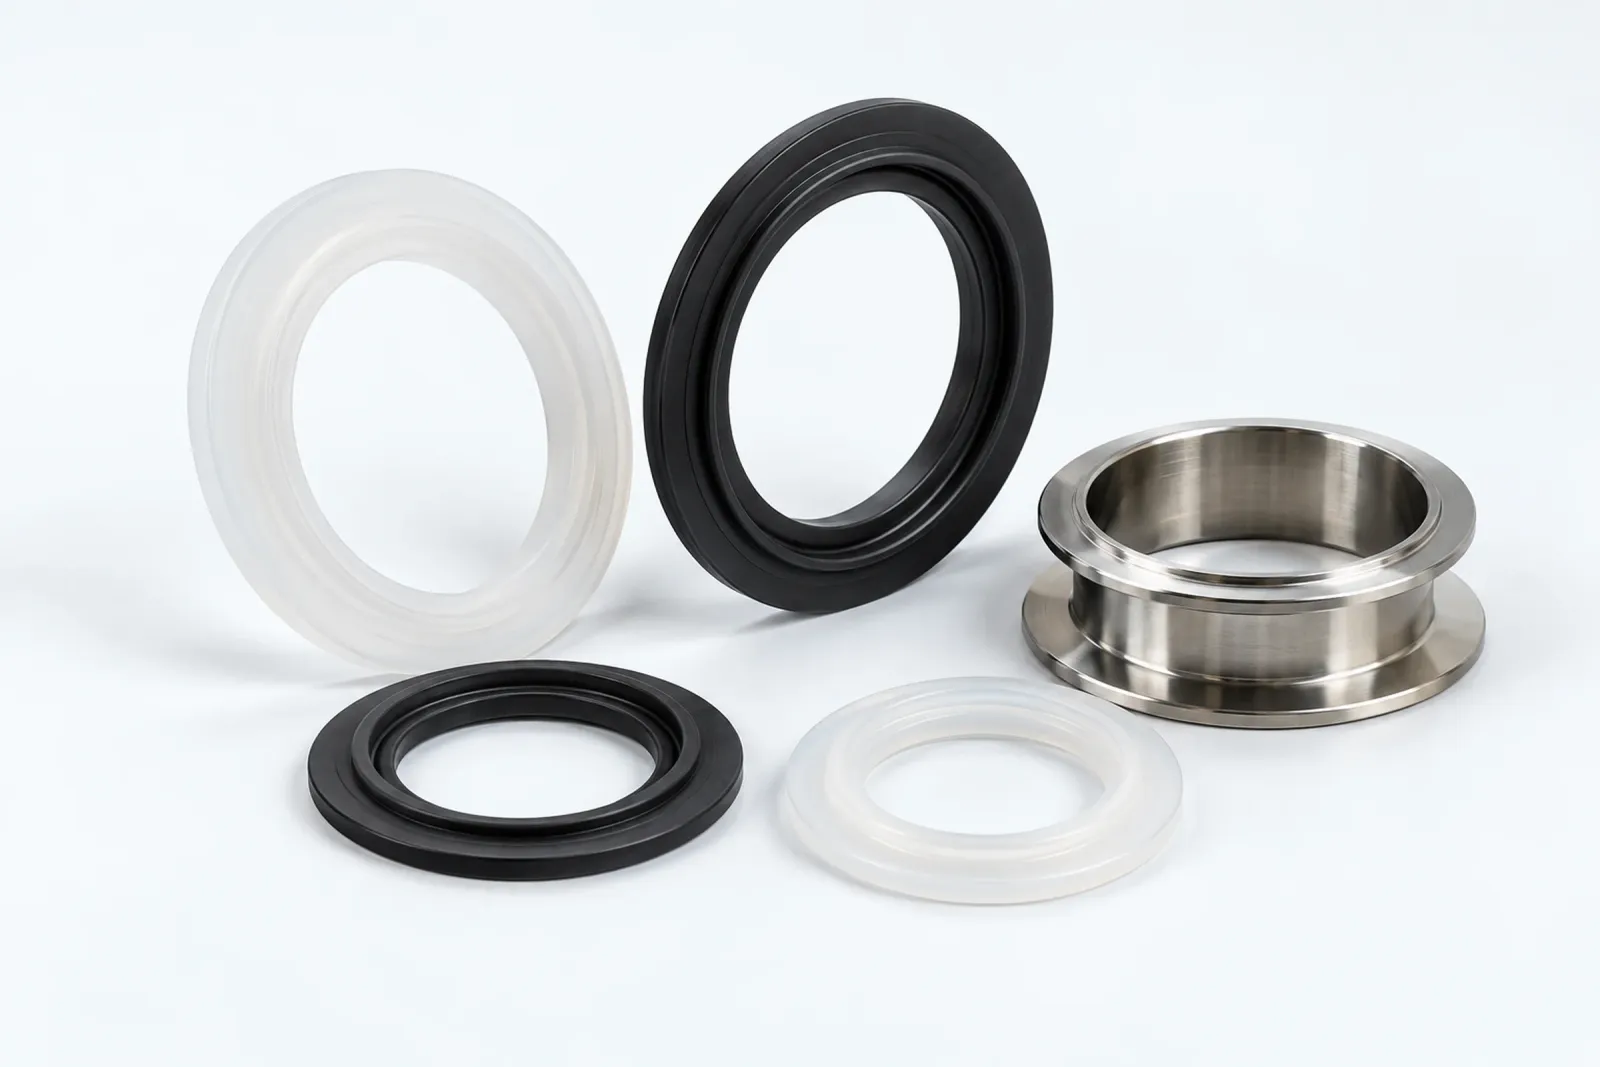
Tri-clamp gaskets that seat between two ferrules on hygienic process pipework and reseal every time the line is opened for cleaning. Moulded to the ferrule sizes of DIN 32676, ISO 2852 or ASME BPE, in EPDM, silicone, NBR or FKM. Dairy screw-coupling seals are made too. Made at our plant in Vilholi, Nashik.
- SEND
- Ferrule standard and size
- STANDARDS
- DIN 32676 · ISO 2852 · ASME BPE (sizing)
- TEMPERATURE
- EPDM to +140 °C; silicone to +200 °C
- FORM
- Moulded
- MADE TO ORDER
- ISO 9001:2015
- 09111526A
Key facts
A sanitary tri-clamp gasket is the moulded rubber ring that seats between two ferrules on hygienic process pipework and reseals each time the line is opened for cleaning. Margo Rubber moulds tri-clamp gaskets to DIN 32676, ISO 2852 or ASME BPE ferrule sizes in Vilholi, Nashik.
Tri-clamp sizes do not all match across DIN 32676, ISO 2852 and ASME BPE, so a gasket made for one can sit proud or short in another. The drawing should name the standard the ferrules were made to. Margo Rubber moulds them in EPDM to +140 °C or silicone to +200 °C.
Product gallery
Visual Reference
What we need from your drawing
- Ferrule standard
- DIN 32676, ISO 2852 or ASME BPE, named on your drawing
- Nominal size
- To the standard
- Bore
- To the standard or your drawing
- Profile
- Flat face with the ferrule-groove bead
Sizing only: the standards fix the dimensions. They do not approve a material, and neither do we by quoting to them.
Technical specifications
Engineering Data
- Product family
- Gaskets
- Material
- EPDM, silicone, NBR, FKM
- Hardness (Shore A)
- To your drawing
- Tensile strength / elongation
- Per compound datasheet, tested to ASTM D412
- Compression set
- Tested to ASTM D395 Method B
- Operating temperature
- By compound; see the table below
- Dimensional standards
- DIN 32676, ISO 2852, ASME BPE
- Colour
- Black standard; other colours on request
- Lead time
- Confirmed with the quotation, from approved drawing and approved sample.
- Certifications
- ISO 9001:2015, certificate 09111526A, Integral Certification Ltd.
- Minimum order
- Set by part size and tooling, quoted with the part. Prototype and first-article lots sit outside it.
Dimensional reference
- Ferrule standard
- DIN 32676, ISO 2852 or ASME BPE, named on your drawing
- Nominal size
- To the standard
- Bore
- To the standard or your drawing
- Profile
- Flat face with the ferrule-groove bead
Available materials
Rubber Compound Options
Select the compound best suited to your operating environment and application requirements.
| Rank | Compound | Temperature | Choose it when |
|---|---|---|---|
| Default | EPDM | −40 to +140 °C | Hot water, steam and CIP. The usual pick for dairy and beverage lines. |
| Leave EPDM if… | the product is fatty or oily | — | Specify NBR (−30/+120 °C). |
| Leave EPDM if… | the line runs dry heat | — | Specify silicone (−60/+200 °C). |
| Leave EPDM if… | the line runs hot acid cleaners or hot oil | — | Specify FKM (−20/+250 °C); not for steam or hot caustic. |
| Also available | AEM (−40 to +160 °C) · Neoprene (CR) (−40 to +120 °C) · SBR (−30 to +100 °C) · Natural rubber (−20 to +90 °C) | See each compound | The rows above are about which one your part needs. |
Not sure? Send the medium, temperature and load
SERVICE RANGE
−40 to +140 °C
EPDM
Key advantages
Why Specifiers Choose Margo
Name the standard
DIN 32676, ISO 2852 and ASME BPE do not match in every size. A gasket cut for one can sit proud or short in another.
Chosen for the wash
Tell us the CIP chemistry and temperature. The wash is often harder on a clamp gasket than the product is.
Moulded, not punched
The groove bead is moulded in, so the gasket locates in the ferrule every time it is refitted.
Tested in-house
Hardness, tensile and compression set in our own lab, with the report in every shipment.
Industries served
Global Applications
Food, Beverage & Pharma
Dairy, brewery, bottling and pharma process pipework
Pumps & Valves
Hygienic pump and valve connections
Manufacturing process
From Compound to Certification
Material compounding
Polymer, fillers and cure system mixed in-house for the medium and temperature on your drawing. Cure is checked on our ODR rheometer.
Tool design
Moulds designed and made for your part and held as a controlled record. When a mould already exists, first samples take 48–72 hours.
Moulding
Compression moulded, with the cavity count set by your volume.
Trimming
Flash trimmed to the edge condition on the drawing.
Inspection
Dimensions against the drawing, hardness and batch sampling. Results go into the shipment documents.
Export packing
Packed by part number with labels that match the inspection sheet. ISPM-15 treated pallets where timber is used.
Quality assurance
Tested in Our Own Lab, Documented in Every Shipment
Every consignment ships with a material test report, a dimensional inspection sheet and a certificate of conformance. Hardness, tensile and elongation (ASTM D412), density, compression set (ASTM D395 Method B), heat ageing, ozone resistance, fluid swell and low-temperature tests run in our own lab, and cure curves run on our own ODR rheometer. PPAP is available on request. RoHS declarations are issued for all compounds.
ISO 9001:2015 · Certificate 09111526A
Integral Certification Ltd
Scope: rubber moulded components — quality management, not a product approval
ISO 9001:2015, certificate 09111526A, Integral Certification Ltd. Scope: rubber moulded components. It certifies the quality management system, not a product approval.
Certification detailProduction metrics
- 60+
- Active clients
- 48–72 hours
- First samples when the mould exists
- 48 hours
- Quotation from receipt of drawing
Downloads
Technical Documentation
Compound datasheets and part drawings are issued on request, under NDA where required.
Request the datasheetFAQ
Technical & Commercial Questions
Answers to the most common questions from engineering teams and procurement managers worldwide.
What is the minimum order for tri-clamp gaskets?
There is no fixed number. The minimum is set by part size and tooling, and we quote it with the part. Send the drawing and your annual volume and you get both figures in one reply. Prototype and first-article lots sit outside the minimum.
Do you stock standard tri-clamp sizes?
No stock range. We mould each size to the standard and drawing you name.
Are your compounds suitable for food contact?
We hold no food-contact certificate for any compound, so food-contact compliance stays with your equipment approval. Tell us the product, temperature and cleaning cycle and we choose the compound for that duty.
Do you send test reports with each shipment?
Yes, with every consignment: material test report, dimensional inspection sheet and certificate of conformance. Hardness, tensile to ASTM D412 and compression set to ASTM D395 Method B are tested in-house.
What are your payment and delivery terms for export orders?
TT and LC, agreed per order. Ex-works Nashik or FOB Nhava Sheva. The commercial invoice, packing list and certificate of origin (Nashik Chamber of Commerce) travel with every consignment.
Related products
You May Also Need
Same compound
Other parts we mould in the same compounds
- EPDM Rotary Shaft Seals — Water, Coolant and Steam · EPDM
- Edge Trim (All-Rubber) — Extruded U-Profiles for Panel Edges · EPDM
- Body Mount Pad — to Suit Mahindra Bolero · EPDM
- Exhaust Hangers & Isolators — Heat-Resistant EPDM, Plain or With Insert · EPDM
- Flat Rubber Washers — Cut or Moulded to Your ID, OD and Thickness · EPDM
- Glove Box Stopper — Damped Interior Closure Bumper · EPDM
Need this part quoted?
Send the ferrule standard and sizes, the product, the cleaning cycle and your annual quantity. We confirm the compound and quote. We respond within 48 hours.